


Experienced aluminum die casting manufacturers usually work with components that need a balance of low weight, structural strength, good thermal conductivity, and production efficiency.
Typical aluminum die cast parts include:
- Motor housings
- Gearbox housings
- Electronic enclosures
- Heat dissipation components
- Mounting brackets
- Automotive structural parts
- Robot components
- Industrial equipment covers
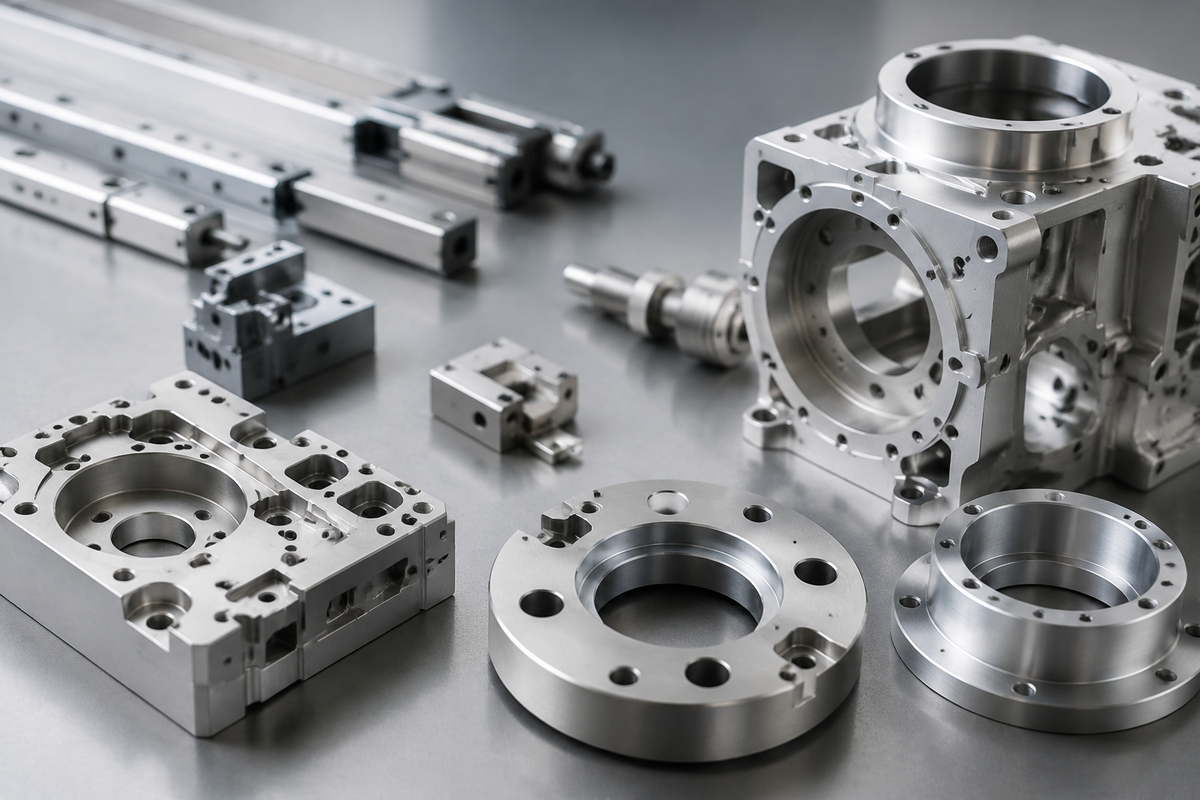
For parts with tight holes, datum surfaces, sealing areas, or precision mounting features, casting is often combined with secondary CNC machining.
Why Supplier Selection Matters
Two die casting suppliers may quote the same drawing very differently.
This does not necessarily mean one quotation is incorrect.
The difference may come from:
- Tooling structure
- Number of cavities
- Mold material
- Expected tool life
- Machine tonnage
- Runner and gate design
- Scrap rate assumptions
- Secondary CNC machining
- Surface treatment requirements
- Inspection standards
- Annual production volume
For this reason, the lowest initial quotation is not always the lowest total project cost.
A capable precision die casting manufacturer should first review how the part will be molded, machined, inspected, and finished before confirming the final production route.

Start With Die Casting DFM
A proper DFM review should happen before tooling starts.
The manufacturer should evaluate wall thickness, draft, ribs, bosses, parting lines, machining allowance, sealing surfaces, and cosmetic areas.
Wall Thickness
Uniform wall thickness improves metal flow and helps reduce shrinkage.
Large thickness changes may create:
- Porosity
- Sink areas
- Incomplete filling
- Local deformation
The appropriate wall thickness depends on the alloy, component size, geometry, and machine capability.
Draft Angles
Draft helps the casting release from the mold.
Insufficient draft can increase:
- Ejection force
- Part deformation
- Mold wear
- Surface damage
External and internal surfaces may require different draft angles.
Ribs and Bosses
Ribs can improve stiffness without creating excessively thick sections.
Bosses are commonly used for:
- Screws
- Threaded inserts
- Alignment
- Assembly points
However, oversized bosses may create local shrinkage or porosity.
Parting Lines
The parting line influences:
- Mold complexity
- Flash location
- Ejection
- Cosmetic surfaces
- Secondary machining
A good custom die casting manufacturer should propose a parting line that balances tool simplicity, casting quality, and functional requirements.

Tooling Is Critical to Casting Quality
The die casting mold directly affects part quality and production stability.
A typical die may include:
- Core and cavity inserts
- Slides
- Lifters
- Ejector pins
- Runner system
- Overflow system
- Cooling channels
- Venting system
For complex components, tooling design can have a greater influence on final quality than the die casting machine itself.
Poor gate or vent design can result in:
- Air entrapment
- Cold shuts
- Porosity
- Incomplete filling
- Flow marks
These issues cannot be solved by inspection alone.
They must be controlled through mold design and process optimization.

Die Casting and CNC Machining
Many industrial components require both die casting and CNC machining.
Die casting produces the near-net shape efficiently, while CNC machining is used only on critical areas.
Common machined features include:
- Precision bores
- Bearing seats
- Threaded holes
- Sealing surfaces
- Datum surfaces
- Tight-tolerance mounting interfaces
- Flatness-critical areas
For example, an aluminum housing may be die cast close to its final geometry and then machined only on mounting faces and bearing bores.
This can significantly reduce machining time compared with producing the entire component from billet.
For this reason, buyers often prefer working with a die casting parts manufacturer that can manage casting and CNC machining under one supply chain.

Precision Die Casting Manufacturer for Tight-Tolerance Parts
Not every feature should be controlled directly by the casting process.
For tighter tolerances, a precision die casting manufacturer should define which dimensions are:
- As-cast dimensions
- CNC-machined dimensions
- CTQ dimensions
- Cosmetic requirements
- Assembly-critical dimensions
Critical areas can then be controlled using machining fixtures, CMM inspection, gauges, or SPC depending on the production volume.
This approach is more practical than applying unnecessarily tight tolerances to every feature on a die cast component.
How Porosity Affects Die Cast Parts
Porosity is one of the main technical considerations in high-pressure die casting.
It may result from:
- Trapped gas
- Shrinkage
- Poor venting
- Improper gate design
- Incorrect process parameters
- Excessive wall thickness
Porosity does not automatically mean that a component is defective.
Its significance depends on the location and application.
For example, internal porosity in a non-critical structural area may be acceptable, while porosity around a sealing face, threaded area, or machined cosmetic surface may create problems.
For pressure-tight parts, manufacturers may use:
- Vacuum-assisted die casting
- Leak testing
- Impregnation
- Optimized venting
- Controlled process parameters
Pressure-sensitive and sealing areas should therefore be clearly identified on the drawing.
Surface Finishing for Die Cast Components
A complete die casting supplier may also coordinate secondary surface treatments.
Common finishing options include:
- Powder coating
- Wet painting
- Anodizing
- Chromate conversion coating
- E-coating
- Sand blasting
- Bead blasting
- Polishing
Surface treatment should be considered during the DFM stage because it can affect:
- Final dimensions
- Appearance
- Corrosion resistance
- Electrical conductivity
- Masking requirements
- Assembly fit
For cosmetic components, the drawing should also define visible surfaces and appearance standards.

How to Evaluate China Die Casting Manufacturers
When comparing China die casting manufacturers, buyers should evaluate technical capability, quality control, production integration, and communication.
Manufacturing Capability
Confirm whether the supplier can handle the required:
- Part size
- Shot weight
- Alloy
- Machine tonnage
- Annual production volume
A supplier focused on small zinc components may not be suitable for large aluminum structural housings.
Tooling Capability
Ask whether tooling design and mold manufacturing are handled internally or outsourced.
Important questions include:
- What mold steel will be used?
- What tool life is expected?
- How many cavities are planned?
- Are slides or inserts required?
- How will gate and venting design be handled?
CNC Machining Capability
If the part contains tight tolerances, check whether CNC machining is available internally.
Integrated casting and machining can reduce tolerance transfer issues and simplify supplier management.
Quality Inspection
Typical inspection equipment includes:
- CMM
- Height gauges
- Micrometers
- Profile projectors
- Surface roughness testers
- Thread gauges
- Leak testing equipment
Inspection requirements should focus on actual CTQ features instead of over-inspecting non-critical dimensions.
Production Capacity
High-volume projects require stable production capacity.
Important factors include:
- Available die casting machines
- Production shifts
- Tool maintenance
- Backup equipment
- Production planning
- Secondary machining capacity
What Affects Die Casting Cost?
Die casting cost normally consists of two main components:
- Tooling investment
- Part production cost
Tooling cost is affected by:
- Part size
- Mold complexity
- Number of slides
- Number of cavities
- Mold steel
- Tool life
- Surface requirements
Part cost is influenced by:
- Material weight
- Cycle time
- Machine tonnage
- Scrap rate
- CNC machining time
- Finishing
- Inspection
- Packaging
- Order quantity
For example, increasing the number of cavities can increase initial tooling cost while reducing the unit cost for larger production volumes.
This is why annual demand should be provided when requesting a quotation from a die casting manufacturer.
Die Casting vs CNC Machining
The most appropriate manufacturing process depends on production volume, geometry, tolerance, and tooling budget.
| Factor | Die Casting | CNC Machining |
|---|---|---|
| Initial tooling cost | High | Low |
| Unit cost at volume | Lower | Higher |
| Prototype flexibility | Lower | Higher |
| Complex molded geometry | Excellent | Depends on tool access |
| Thin walls | Good | More difficult |
| Tight tolerances | Often requires CNC finishing | Excellent |
| High-volume production | Excellent | Less economical |
For low-volume prototypes, CNC machining may be more practical.
Once production volume increases, die casting can reduce material waste and cycle time.
Many projects therefore begin with CNC prototypes before transitioning to custom aluminum die casting for mass production.

Why Use One Die Casting Parts Manufacturer?
Using separate suppliers for casting, CNC machining, surface treatment, inspection, and assembly can increase coordination complexity.
A vertically integrated die casting parts manufacturer can manage:
Tooling → Die Casting → Trimming → CNC Machining → Surface Finishing → Inspection → Assembly
This approach can improve:
- Dimensional consistency
- Responsibility control
- Lead time
- Traceability
- Engineering communication
- Quality issue resolution
It is especially useful for parts with multiple datums, tight machining requirements, cosmetic surfaces, or assembly operations.
Information Needed for a Die Casting Quote
To obtain an accurate quotation, provide as much project information as possible.
Recommended information includes:
- 3D CAD model
- 2D drawing
- Material specification
- Surface treatment
- Critical tolerances
- Annual production volume
- Initial order quantity
- Cosmetic requirements
- Assembly requirements
STEP, STP, or Parasolid files are normally suitable for DFM review.
PDF drawings should clearly identify critical dimensions, tolerances, and surface requirements.
FAQ
How do I choose reliable die casting manufacturers?
Evaluate tooling capability, die casting machine range, CNC machining, inspection equipment, material experience, quality systems, and production capacity instead of comparing price alone.
What should I look for in aluminum die casting manufacturers?
Check whether the supplier has experience with similar component size, alloy, wall thickness, machining requirements, cosmetic standards, and expected production volume.
Can a custom die casting manufacturer also provide CNC machining?
Yes. Many custom manufacturers combine die casting with CNC machining for bores, threads, datum surfaces, sealing faces, and precision mounting features.
Is China suitable for custom die casting production?
China has a large die casting supply base covering tooling, casting, machining, finishing, and assembly. Supplier capability varies significantly, so technical evaluation and DFM review are important before tooling begins.
What is the advantage of using one die casting supplier?
A single supplier managing casting, machining, finishing, and inspection can reduce coordination effort and improve traceability throughout production.
Custom Die Casting Manufacturing at XY-GLOBAL
When selecting die casting manufacturers, it is important to evaluate more than casting capacity alone.
Tooling design, CNC machining, process control, surface finishing, and inspection all influence whether the final component meets production requirements.
As a custom die casting manufacturer, XY-GLOBAL supports aluminum and zinc die casting projects from DFM and tooling through CNC machining, finishing, inspection, and assembly.
We support prototype validation as well as volume production for industrial equipment, robotics, electronics, automotive, and other precision applications.
If you are comparing aluminum die casting manufacturers or looking for a reliable die casting supplier for a new project, send us your 2D drawing, 3D model, material requirement, and expected production quantity. Our engineering team can review the design before tooling begins.

Share:
Stamp and Preform Manufacturing for Precision Components